ZhongZe
China RotoMolds & OEM
Get a Quote
ZhongZe
China Roto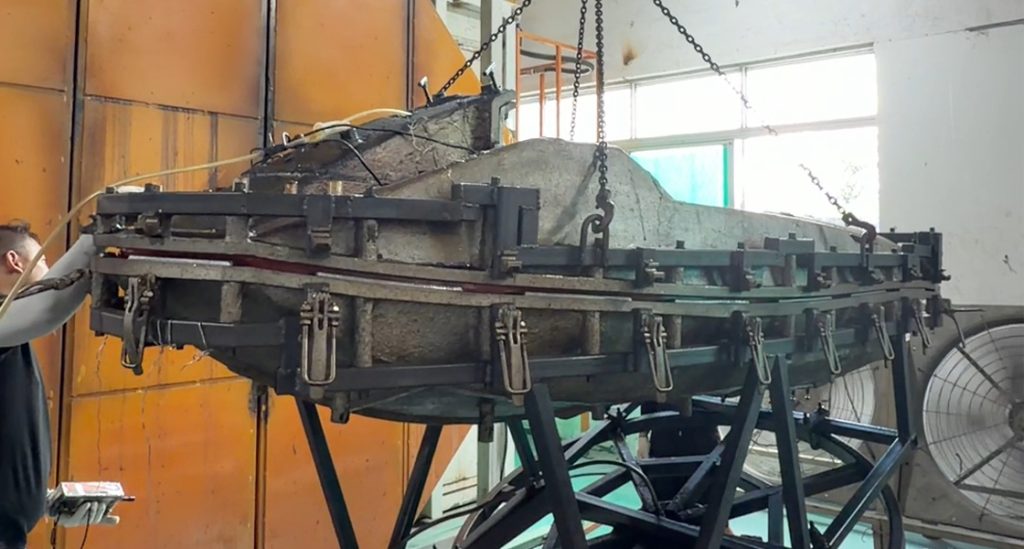
Mold venting is a basic requirement in rotational molding. During molding, the mold is heated and rotated while the polymer material builds up on the inside surface of the mold. The mold needs a suitable venting path to prevent unwanted pressure from developing inside the cavity.
Venting should therefore be considered as part of the mold design, together with product geometry, mold volume, material loading, and the intended molding process.
Rotational molding is a low-pressure process, but the mold is not operated as a sealed pressure vessel.
ARM states that most rotational molding parts require an opening through the mold wall to accommodate a vent pipe. The purpose is to prevent the mold from becoming pressurized during the molding cycle. ARM also notes that large, flat, unsupported surfaces should be vented to help minimize warpage and potential mold damage.
The vent therefore needs to remain functional throughout heating, rotation, and cooling. A restricted or blocked vent can change the pressure conditions inside the mold.
Vent size should not be selected from a single fixed dimension for every mold.
ARMA provides a practical guideline of 13 mm vent tube diameter for each 1 m³ of mold volume. This is a guideline rather than a universal specification, and the actual vent arrangement depends on the mold and production conditions.
For example, a large mold cavity requires more attention to vent capacity than a small mold. Vent design also needs to account for the way the mold is loaded and rotated.
The guideline should therefore be treated as a starting point for engineering review, not as a substitute for mold-specific design.
A vent is not simply a hole through the mold wall.
The vent tube needs to provide communication between the mold cavity and the surrounding atmosphere while preventing polymer material from escaping during rotation. ARMA specifically notes that the vent tube should extend sufficiently through the powder pool to prevent material from entering the tube during molding.
ARM also notes that the required size and location of vents should be considered during detailed product design. In some applications, a vent opening can be positioned in an area that will later be removed or incorporated into a required product opening.
This makes vent location both a mold-design and product-design consideration.
Product geometry affects mold volume and the way the mold is loaded and operated. Deep or complex sections, large unsupported surfaces, and other restricted geometries may require closer review during mold development.
Venting should not, however, be treated as a way to correct every molding problem. Powder flow, material loading, heating, rotation, cooling, and product geometry can all affect the molded part. ARM’s design guide, for example, identifies restricted powder flow as a cause of bridging in closely spaced or complex sections.
A venting issue and a material-distribution issue should therefore be evaluated separately before making a process or mold modification.
The final venting arrangement should be verified under actual production conditions.
During a mold trial, the molder can check mold operation and the resulting part, including dimensions, wall thickness, weight, appearance, and other product-specific requirements. If a problem is found, venting should be considered together with the other relevant mold and process conditions rather than changed automatically.
This approach is particularly important because rotational molding involves both material and thermal behavior. ARM notes that polyethylene parts can experience approximately 1–4% shrinkage, depending on related factors, and that differential shrinkage can contribute to warpage.
For a custom rotomolding mold, venting should be established from the mold volume, product geometry, material loading, vent location, and production method.
The 13 mm per 1 m³ figure published by ARMA is useful as an industry guideline, but it should not be presented as a universal vent specification. Final vent design needs to be checked against the actual mold and molding process.
Rotational molding mold and OEM manufacturing insights, covering mold development, materials, design and production.
Need a custom mold, OEM production, or an electric kart boat? Share your project details with us. Our team will review your requirements and get back to you promptly.
No drawings yet? We can help review your idea and recommend the right approach.